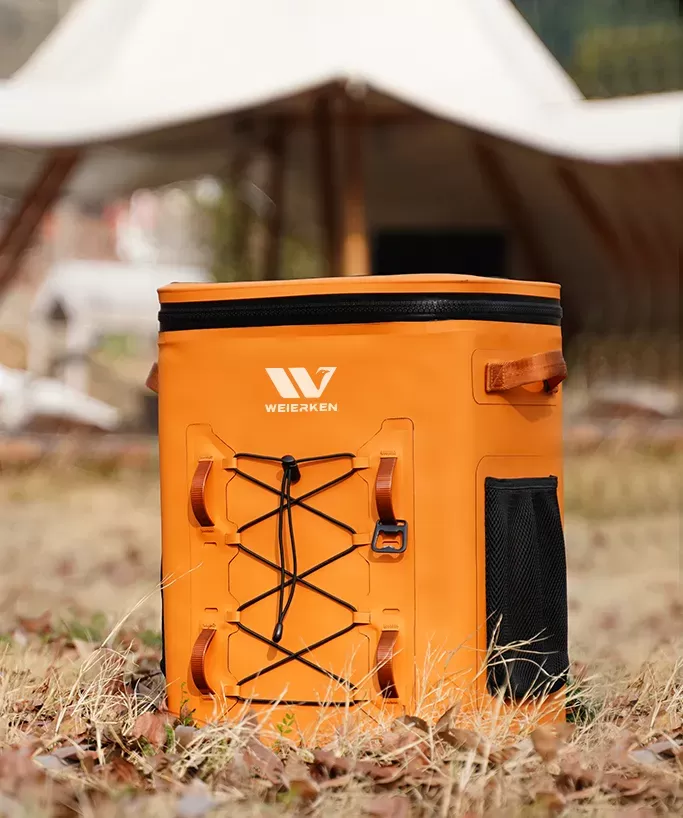


High-end chocolate is fragile. When ambient temperatures rise above 24°C, cocoa butter begins to soften. At 28°C to 32°C, the crystal structure collapses entirely. Once that happens, fat bloom ruins the product's finish, texture, and snap.
A single temperature excursion during last-mile delivery or regional distribution can destroy tens of thousands of dollars in finished stock. Standard retail picnic bags cannot protect confectionery against these shifts. Professional confectionery logistics requires structural insulation, reflective thermal barriers, and air-tight engineering.
If you source cold-chain packaging for a confectionery brand, selecting the right partner is vital. Many factories claim they produce cold-chain gear, but they often just repurpose low-density grocery totes. Companies like Weierken design dedicated solutions built for temperature-sensitive confectionery, proving that specialized engineering matters.
This audit guide walks through a step-by-step technical framework to evaluate an OEM chocolate transport cooler bag supplier before issuing your next purchase order.
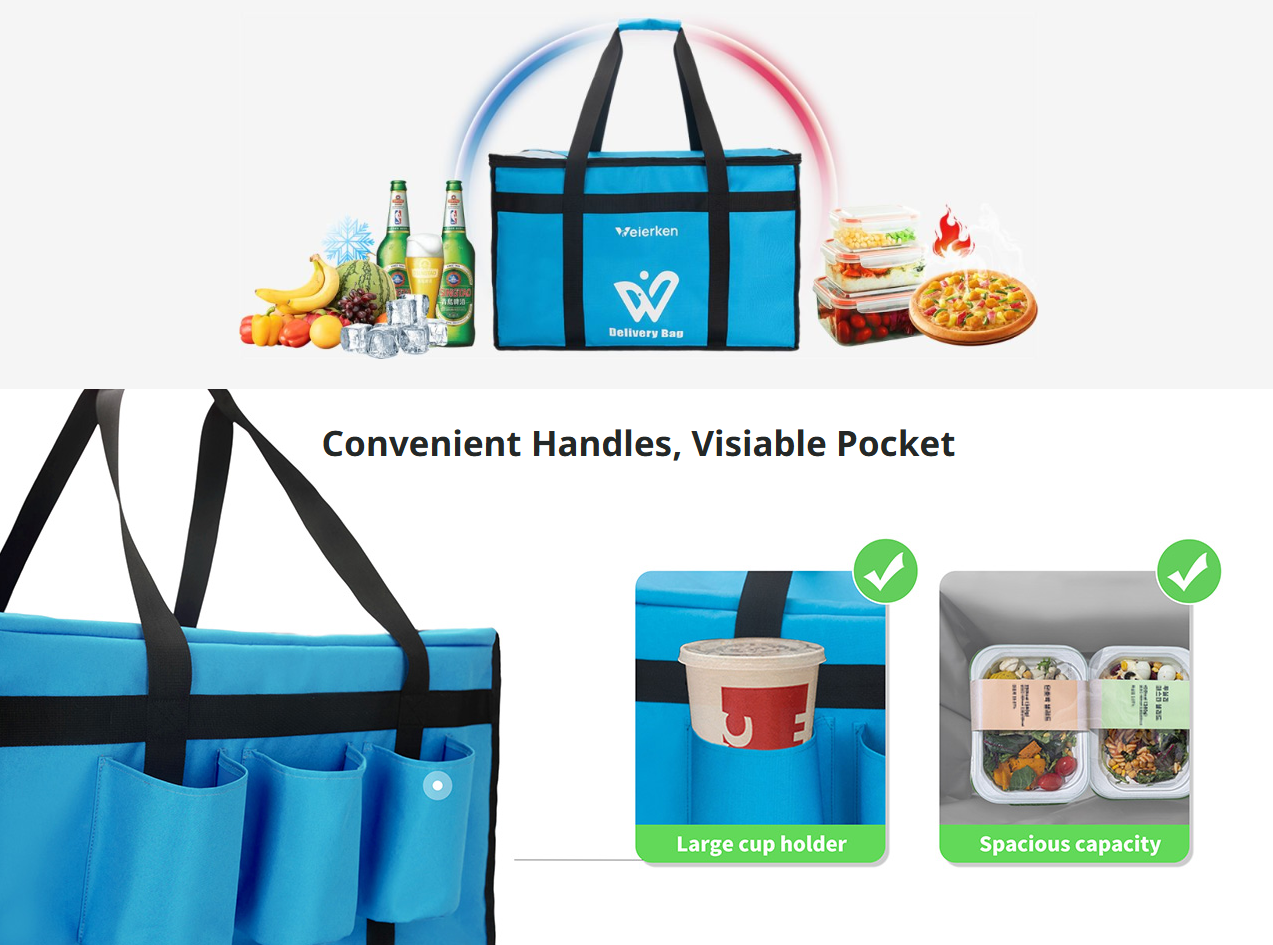
Module 1: Thermal Engineering & Material Audit
Thermal packaging relies on basic physics: conduction, convection, and radiation. An unverified supplier will likely use whatever scrap materials they have on hand. Your audit must verify every layer of the thermal sandwich.
Insulation Cores: Evaluating Thermal Resistance (R-Value)
The insulation core controls conductive heat transfer. You should request raw material spec sheets for the bag's interior layers. Common options vary widely in performance:
Standard EPE Foam (Expanded Polyethylene): Low cost, but collapses under pressure. It provides poor thermal resistance (R-value) over transit times exceeding 4 hours.
High-Density XPE Foam (Cross-linked Polyethylene): Closed-cell structure with much higher rigidity. It resists repeated compression and maintains consistent wall thickness under payload weight.
Polyurethane (PU) Foam: Offers superior insulation for mid-range durations (12 to 24 hours), though it adds bulk to flat-pack shipping.
Vacuum Insulation Panels (VIP): The gold standard for multi-day logistics. VIPs deliver the highest thermal resistance with minimal thickness, keeping interior chocolate stable across long transit routes.
Radiation Barriers: Pure Aluminum Foil vs. VMPET
Confectionery shipments often sit on sunny tarmac strips or inside unconditioned delivery vans. Radiant heat barrier selection makes a measurable difference:
VMPET (Metalized Polyester): A thin plastic film coated with a microscopic layer of aluminum. It reflects some radiant heat, but tears easily and degrades under friction.
Pure Aluminum Foil Laminate: Reflects up to 97% of radiant heat. When bonded to high-density XPE or woven fabric, it creates an impermeable barrier against radiant heat and humidity.
Ask your chocolate transport cooler bag supplier for material composition reports. If they substitute pure foil with cheap metalized film without your approval, your shipments will suffer during summer heat spikes.
Airtightness & Closure Engineering
Convective heat transfer occurs when cold air leaks out and warm, moist air enters the bag. Standard nylon coil zippers allow significant air exchange. Moisture then condenses inside the cavity, degrading paper packaging and causing sugar bloom on the chocolate.
Examine how the factory handles seals. Look for high-frequency RF (radio-frequency) welded seams instead of standard stitch lines. For high-value shipments, check if they can integrate waterproof, airtight zippers (such as TPU-coated teeth) to keep the thermal payload completely sealed.
Phase Change Material (PCM) Integration
Chilled chocolate should rarely touch bare ice packs. Direct contact with water-based ice freezes the chocolate, which creates sugar bloom once the surface warms up. A professional supplier understands this issue.
Verify whether the factory can build dedicated divider sleeves, internal mesh suspension pockets, or baffling systems. These compartments hold 14°C to 18°C phase change materials (PCMs) away from the product, surrounding the chocolate with stable ambient cold rather than freezing cold.
Module 2: Food Safety & Compliance Verifications
Cocoa butter absorbs surrounding odors rapidly. If an insulated bag contains volatile organic compounds (VOCs) from cheap glues or recycled plastics, the chocolate will pick up that chemical smell before delivery. Strict material safety audits are non-negotiable.
Lining Material Certifications
The interior liner must have documented food-contact approval, even if the chocolate has primary packaging. Secondary leaks or condensation can spread contaminants throughout the bag interior.
FDA 21 CFR Compliance: Ensures the lining material contains no toxic plasticizers or heavy metals.
LFGB / REACH Compliance: Crucial for European distribution. Confirms the materials will not transfer odors, tastes, or hazardous substances to edible products.
Antimicrobial and Anti-Mildew Treatment: Condensation happens inside cold packs. The inner lining (such as food-grade TPU or PEVA) needs antimicrobial additives to stop mold growth during return logistics or multi-use routes.
Facility Standards and Social Compliance
Audit the factory's certifications to ensure they can meet international trade requirements:
ISO 9001: Verifies basic quality management and process controls.
BRCGS Packaging Materials: An excellent indicator that the plant follows high cleanliness standards suitable for the food supply chain.
BSCI / SEDEX (SMETA): Verifies labor standards and worker safety. Global retailers will reject suppliers who fail social compliance audits.
Module 3: Factory Production Capacity & Lab Testing Capabilities
Many trading brokers claim to be manufacturers. A real chocolate transport cooler bag supplier maintains on-site assembly equipment, quality control stations, and testing setups.
Experienced manufacturers like Weierken run structured testing to balance insulation efficiency with production yield. When you inspect an OEM facility, ask to review their quality lab.
The Thermal Test Chamber
A reliable supplier does not guess how long a cooler bag maintains internal temperatures. They run tests in a programmable environmental chamber that mimics target transit routes.
Ask the supplier to provide thermal decay curve reports showing:
Internal payload temperature held between 15°C and 20°C.
External ambient chambers set to sustained heat (e.g., 35°C to 40°C).
Thermal performance tracked over 12, 24, 48, or 72 continuous hours.
If the supplier cannot share actual data logger graphs, they are relying on guesswork rather than cold chain engineering.
Mechanical QC Checkpoints
A cooler bag must survive physical impacts across warehouses and parcel networks. Review their on-site physical testing gear:
Tensile Strength Testers: Measure stitch integrity at handle load points to prevent transit failures.
Zipper Reciprocating Testers: Cycle closures hundreds of times to confirm zipper teeth and slide pullers do not jam.
Drop Tests: Bags packed to maximum gross weight are dropped from 1 to 1.5 meters to verify seam strength.
Hydrostatic Leak Testing: Confirms heat-sealed liners stay leakproof if ice packs condense or rupture.
Module 4: OEM/ODM Customization & Structural Flexibility
Every confectionery line uses different packaging. A subscription artisan box needs a different form factor than a commercial 5 kg couverture block shipment. Your supplier must offer flexible, tailored designs.
Form Factor and Dimensional Customization
Ensure the supplier can build custom samples to match your secondary packaging:
Collapsible Flat-Pack Designs: Reduces inbound freight volume and cuts storage costs in fulfillment centers.
Rigid Box Inserts: Self-erecting insulated panels fitted into corrugated cartons for automated packing lines.
Tote Formats: Designed for local direct-to-consumer couriers with quick velcro closures.
Branding Techniques Without Thermal Degradation
Branding matters, but traditional production steps can compromise a bag's insulation. For example, deep machine embroidery punches thousands of needle holes through insulation layers, causing cold air leaks.
Check if the factory uses non-invasive decoration methods. Reliable options include silk-screen printing with food-safe inks, heat-transfer films, high-frequency embossing, or attaching badging only to the outer fabric shell before insulating the core.
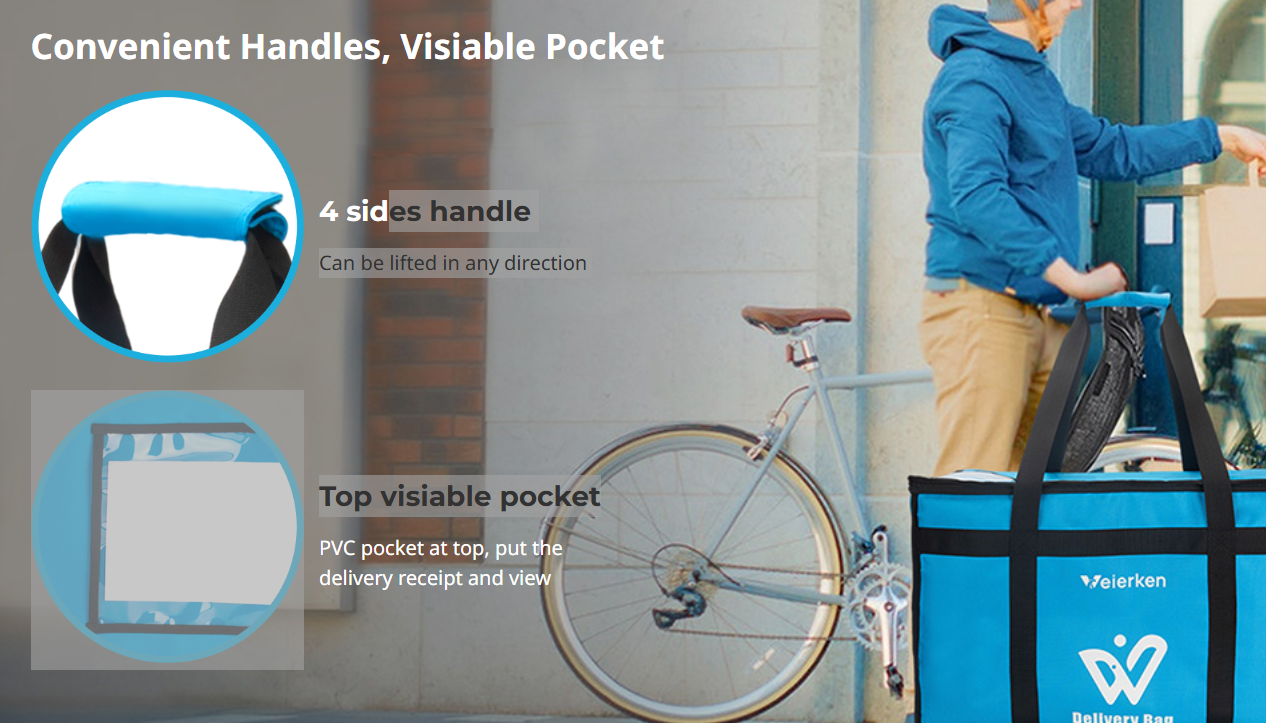
Module 5: Supply Chain Resilience & Peak Season Execution
Confectionery logistics peaks around specific calendar events: Valentine’s Day, Easter, Halloween, and Christmas. Your supply chain cannot afford delivery delays during these periods.
Raw Material Stocking and Buffer Management
Ask prospective vendors how they manage inventory ahead of production spikes. Do they maintain safety stock for high-density foam, aluminum laminates, and zippers? If an OEM waits for your deposit before ordering basic raw materials, lead times can easily double during peak Q3 and Q4 runs.
Subcontracting Risks
Mid-tier factories often accept large purchase orders during peak season, only to quietly outsource production to unqualified workshops. This introduces defects, inconsistent insulation, and unwashed linings.
Demand transparency. Your supply agreement should require explicit written approval before any production can move to a secondary site, backed by unannounced third-party inspections.
Supplier Audit Checklist for Chocolate Cooler Bags
Use this practical checklist when reviewing quotes and auditing potential manufacturing partners:
[ ] Core insulation uses high-density XPE, PU, or VIP (not low-density EPE foam).
[ ] Reflective layer uses pure aluminum foil laminate for maximum radiant heat reflection.
[ ] Inner liners have certified food-contact documentation (FDA / LFGB) with low odor emission.
[ ] High-stress joins use leakproof welded seams instead of through-stitch sewing.
[ ] Factory operates an on-site thermal chamber and can provide temperature decay graphs.
[ ] Mechanical testing confirms handle tensile strength, zipper lifespan, and seam durability.
[ ] Factory holds valid ISO 9001 and social responsibility audits (BSCI, SEDEX).
[ ] Clear seasonal capacity planning ensures no unauthorized subcontracting during peak quarters.
Frequently Asked Questions
Q1: Why can't we use standard supermarket cooler bags for chocolate transport?
A1: Standard retail cooler bags rely on thin, low-density EPE foam and stitched seams. They leak air constantly and cannot stop radiant heat. Chocolate melts easily and develops fat bloom when exposed to small temperature swings. Professional cold-chain bags use higher-density insulation, sealed seams, and radiant foil barriers to keep internal temperatures between 14°C and 18°C for extended periods.
Q2: How do we prevent condensation from ruining artisan chocolate packaging inside the bag?
A2: Condensation occurs when warm outside air mixes with cold air inside the bag. You can prevent this by pairing airtight, water-resistant closures with specialized phase change materials (PCMs) rated for 14°C to 18°C, rather than traditional sub-zero water ice packs. Compartmentalized pockets keep cold sources separated from retail boxes, protecting the paper packaging from humidity.
Q3: What is the typical Minimum Order Quantity (MOQ) for an OEM chocolate cooler bag?
A3: MOQs generally range from 500 to 2,000 units, depending on customization depth. Off-the-shelf fabrics with simple logo prints have lower thresholds. Fully custom dimensions, custom-dyed fabrics, or high-frequency welded TPU liners typically require 1,000 to 3,000 units to offset machine setup and raw material extrusion runs.
Q4: How long can a professionally engineered cooler bag maintain the 15°C–18°C range?
A4: Performance depends on wall thickness, insulation material, refrigerant mass, and ambient temperatures. A well-designed bag using high-density XPE foam and pure aluminum foil holds stable temperatures for 12 to 24 hours in standard summer logistics. Upgrading to thicker PU panels or vacuum insulation panels (VIP) extends that protection past 48 to 72 hours.
Q5: How can we tell if a factory's lining material will leave an odor in our chocolate?
A5: Request a raw material sample and run an odor-transfer test. Place the lining material in an airtight glass jar with unscented chocolate buttons or pure cocoa butter for 48 hours at 25°C. Taste and smell the sample against an isolated control piece. You should also request certified LFGB or FDA reports confirming low VOC content.
Conclusion: Protecting Your Brand Value
Cutting corners on cold-chain packaging rarely saves money. A single spoiled production run ruins retail relationships and hurts brand reputation. Evaluating a potential chocolate transport cooler bag supplier on thermal engineering, material safety, and testing capabilities ensures your products arrive in perfect condition.
Working with an experienced manufacturer like Weierken helps eliminate cold chain risks through verified materials and controlled factory production. Protect your product quality, reduce transit spoilage, and maintain customer satisfaction year-round.
Need to validate your cold-chain logistics? Contact our technical packaging team today to review custom samples, evaluate temperature decay data, or request a quote on custom OEM cooler bags built for confectionery shipping.