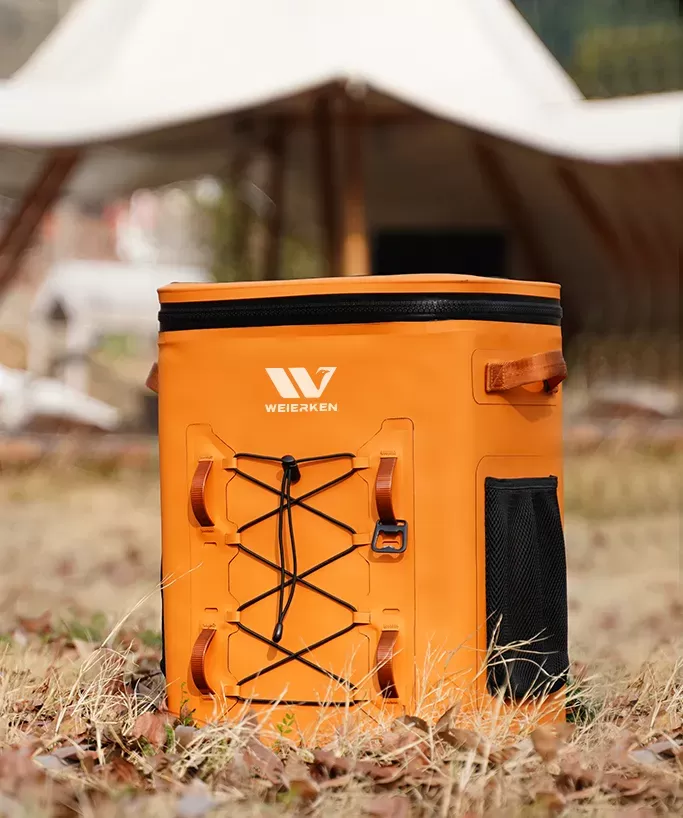

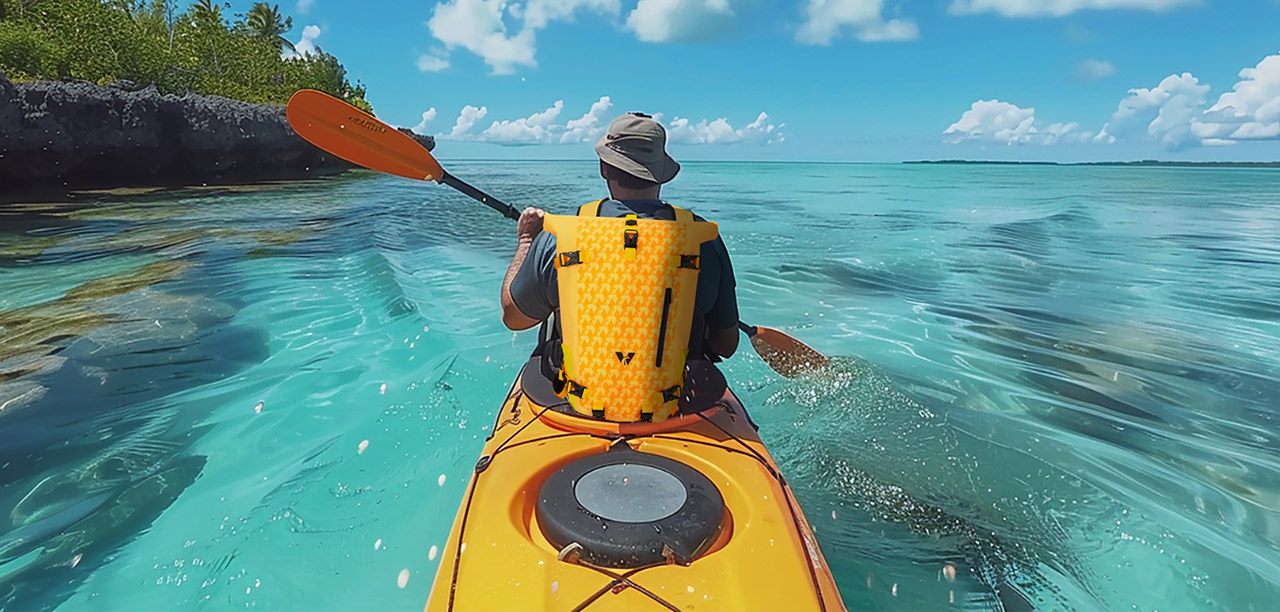
Paddlesport gear is moving away from generic dry sacks. Kayakers, packrafters, and touring paddlers now demand purpose-built gear: deck bags with quick-access hatches, tapered bow and stern float bags, and waterproof cockpit organizers that survive coastal exposure.
For outdoor brands and sourcing directors, changing factories carries heavy operational risks. A bad manufacturing partner creates leaking seams, customer returns, customs seizures over chemical regulations, and late delivery dates during peak paddling season. Choosing a dedicated custom kayak dry bag manufacturer requires evaluating technical engineering rather than accepting low bids. OEM/ODM specialists like Weierken build gear to survive actual coastal expeditions, proving that production methods dictate your warranty return rate.
1. Technical Sealing Capabilities: General Bags vs. Kayak-Specific Gear
A basic dry bag relies on stitched seams with glued PU tape. This method fails quickly in marine environments. Constant water pooling on a kayak deck breaks down adhesive glue lines, while cockpit friction shreds standard taped joints.
High-Frequency (RF) Welding Over Taped Seams
Professional marine gear requires radio frequency (RF) welding or hot-air sealing. RF welding passes electromagnetic energy through compatible thermoplastic films, fusing the molecular chains together. The bond becomes a monolithic barrier rather than two pieces glued together.
- Seam Tensile Strength: Welded seams retain up to 95% of the base fabric strength, compared to roughly 50% for stitched and taped alternatives.
- Chemical Longevity: Welded bonds do not hydrolyze or peel when exposed to continuous moisture, saltwater, and cockpit sunscreen oils.
- Ultrasonic Sealing: Experienced factories apply ultrasonic welding for tight curves, such as contoured deck bag perimeters and lash tabs.
Air-Tight and Watertight Zip Systems
If your designs call for splash-proof pockets or full IPX7 submersion, seam construction is only half the battle. Your custom kayak dry bag manufacturer must have proven experience integrating airtight zippers (such as TIZIP or airtight YKK systems).
Installing these heavy-duty zippers requires precise heat-welding fixtures. If the fabric overlaps unevenly by even a single millimeter, the zip teeth misalign, causing air leaks and water ingress under hull pressure.
2. Material Selection and the 2026 Sustainability Shift
Environmental regulations and buyer expectations are transforming performance fabrics. Brands must balance technical durability with strict chemical compliance.
The Move from PVC to Technical TPU
Polyvinyl chloride (PVC) dominated entry-level dry sacks for decades due to low raw material costs. However, technical paddlesport brands are systematically eliminating PVC for high-end kayak bags for several functional reasons:
- Cold-Crack Resistance: Thermoplastic polyurethane (TPU) remains flexible at temperatures well below freezing, whereas PVC stiffens and cracks when handled roughly in cold water.
- Abrasion and Puncture Resistance: A 420D nylon backed with double-sided TPU provides superior puncture resistance against kayak bulkheads, sand, and sharp deck hardware at half the weight of heavy PVC.
- Environmental Toxins: TPU contains no volatile plasticizers, ensuring it does not leach toxic phthalates into sensitive aquatic ecosystems.
PFAS-Free and GRS Certifications
Regulatory compliance is an urgent sourcing challenge. The European Union and multiple US states now enforce strict bans on intentionally added per- and polyfluoroalkyl substances (PFAS) in outdoor equipment. Importing textiles with fluorinated DWR coatings will lead to port rejections and massive fines.
Your manufacturer must provide verifiable testing certificates proving their durable water-repellent (DWR) formulations are 100% PFC/PFAS-free. Leading factories also support Global Recycled Standard (GRS) post-consumer recycled fabrics (RPET), allowing brands to hit ESG benchmarks without sacrificing tear resistance.
3. Kayak-Specific Structural Engineering
A true custom kayak dry bag manufacturer understands that water on a kayak acts dynamically. High-volume rolling waves, cockpit wash, and UV exposure place unique mechanical loads on gear.
Deck-Rigging Hardware and Salt-Spray Defense
Corrosion destroys field utility. Normal steel or cheap electroplated hardware oxidizes rapidly after exposure to saltwater spray. Ensure your supplier works with:
- POM / Acetal Buckles: Specialized plastic hardware (from suppliers like Duraflex or ITW Nexus) that resists UV degradation and maintains latching strength when caked with marine salt.
- Marine-Grade Stainless Steel: If metal D-rings are used, demand 316-grade stainless steel passed through rigorous ASTM B117 salt spray chamber tests.
- Reinforced Hypalon Lash Patches: Deck bags sit under constant tension from bungee cords. Heavy lash points should be RF-welded with backing plates to prevent fabric tear-out.
Contoured Hull and Deck Patterning
Generic cylindrical bags waste hull volume. Sourcing teams should seek factories capable of complex 3D patterning. Bow and stern hatch compartments taper rapidly, meaning float bags must mirror hull deadrise. Specialized engineering partners like Weierken utilize precision CAD tooling to create bespoke, three-dimensional shapes that fit snugly inside bulkheads or lay flush against sit-inside cockpits.
4. Customization, Tooling, and Prototyping
Turning a tech pack into a market-ready production run requires an active Design for Manufacturability (DFM) process. A factory should not simply follow drawings blindly; they should optimize them for high manufacturing yields.
- Tooling and Welding Horns: Welded shapes require custom aluminum or brass dies. Clarify tooling costs early. The supplier should build durable tooling that lasts through tens of thousands of production cycles.
- Marine-Grade Printing: Standard screen printing peels off slick TPU and silicone coatings. Ask for high-adhesion inks, vulcanized transfer prints, or laser etching that withstands continuous salt scrub and UV exposure.
- Air Release Valves and Windows: Kayak gear often benefits from built-in compression valves to squeeze excess air from tight hulls, or clear TPU windows to inspect interior contents without opening the bag.
- Prototyping Speed: Professional factories deliver functional prototypes within 7 to 14 working days, refining seam allowances and valve locations before cutting production dies.
5. Factory Quality Assurance and Compliance Audits
A waterproof bag that fails in mild chop damages your brand reputation. Sourcing managers must demand strict quality verification protocols directly on the factory floor.
In-House Testing Protocols
A reputable factory should not rely on visual inspection alone. They must maintain a dedicated QC laboratory equipped for specific marine testing:
- Submersion Testing (IPX7 / IPX8): The bag is submerged in a water tank at specified depths (typically 1 meter for 30 minutes) to confirm that airtight zippers and seams withstand hydrostatic pressure.
- Hydrostatic Head Testing: Measures the millimeters of water column pressure the base fabric and seams survive before moisture penetrates (standard performance demands >10,000mm).
- Air Inflation Retention: Technicians pressurize completed bags to 1.5–2.0 PSI and monitor pressure drops over a 24-hour cycle to catch micro-leaks along welded corners.
- Tensile and Shear Tests: Seams are pulled apart on calibrated tensile testing machines to verify bonding consistency across different roll batches.
Essential Factory Certifications
Protect your brand from labor scandals and border seizures by verifying external certifications:
- Social Compliance: BSCI, Sedex (SMETA), or SA8000 audit reports verifying fair labor practices, safe workshop environments, and ethical operations.
- Quality Management: ISO 9001 certification demonstrating stable process controls from raw material incoming inspection (IQC) to final shipment inspection (FQC).
- Chemical Safety: REACH, RoHS, and Prop 65 compliance
documentation covering all plasticizers, dyes, and coatings.
6. Supply Chain Economics: Red Flags to Watch Out For
Cost per unit is critical, but chasing the cheapest factory often results in hidden expenses down the line. Keep watch for these common supply chain warning signs:
- Subcontracted Welding: Some factories accept dry bag orders but lack internal RF welding capacity. They cut fabric in-house and subcontract the welding to small workshops. This breaks quality traceability and ruins lead-time accuracy.
- Vague Raw Material Documentation: If a supplier cannot present Certificates of Analysis (COA) for TPU coating thickness or fabric denier, they may be blending sub-prime resin, which leads to early delamination.
- Ambiguous Mold Ownership: Ensure your manufacturing agreement clearly states that all custom tooling, welding dies, and injection molds paid for by your company remain your exclusive intellectual property.
- Rigid Minimum Order Quantities (MOQs): Inflexible MOQs kill new product experimentation. A progressive manufacturing partner offers tiered MOQs (e.g., lower initial runs for custom colorways, higher runs for core SKUs) to help you manage working capital.
Frequently Asked Questions
Q1: What is the main difference between TPU and PVC for kayak dry bags?
TPU (Thermoplastic Polyurethane) is lighter, remains flexible in near-freezing water, and delivers significantly higher abrasion resistance than PVC. It is also more environmentally sustainable and free from toxic plasticizers, making it the preferred choice for technical outdoor brands despite a slightly higher raw material cost.
Q2: Why is radio-frequency (RF) welding required for kayak dry bags?
RF welding fuses thermoplastic materials at the molecular level without thread holes or glue. Glued seams degrade when exposed to continuous moisture, saltwater, and heat, whereas an RF-welded seam creates an impermeable, permanent barrier that will not delaminate or leak.
Q3: What IPX rating should I require for a technical kayak deck bag?
For deck bags exposed to heavy spray and occasional wave overtopping, an IPX6 rating (protection against heavy seas and powerful water jets) is standard. For hatch bags, cockpit bags, or cases intended for electronics that might face full submersion during a capsize, demand an IPX7 (submersion up to 1 meter for 30 minutes) or IPX8 rating.
Q4: How long does the prototyping process take for a custom kayak bag?
Standard prototyping typically takes between 7 and 15 business days, depending on pattern complexity. If your design requires custom injection molds for hardware or bespoke RF welding dies, initial tooling fabrication may add an extra 2 to 3 weeks.
Q5: How will 2026 PFAS regulations affect custom dry bag manufacturing?
Import regulations in the US and Europe now ban or severely restrict intentionally added PFAS/PFCs used in traditional durable water-repellent (DWR) coatings. Sourcing directors must ensure their manufacturer uses verified PFAS-free DWR finishes and can provide full lab testing documentation to clear customs inspection.
Choose an Engineering Partner, Not Just a Vendor
Building high-performance kayak accessories requires deep technical alignment. The ideal factory acts as an extension of your product design team, proactively catching weak stress points, navigating chemical bans, and ensuring every seam passes pressure verification.
Experienced technical manufacturers like Weierken help outdoor brands launch robust, market-ready watersports gear while staying fully compliant with modern environmental standards. If you want to refine an existing technical pack or develop an entirely new kayak line for the upcoming season, start with an engineering-focused evaluation.
Ready to elevate your paddlesport product line? Send your tech pack to our engineering team today to request a comprehensive DFM review, review material swatches, and receive a competitive manufacturing quote.